From easy quoting to quick-turn production and finishing options, get up to 500 quality sheet metal parts in your hands in days from a single supplier.
Relevant Certificates
Quality documentation and certificate support
From easy quoting to quick-turn production and finishing options, get up to 500 quality sheet metal parts in your hands in days from a single supplier.
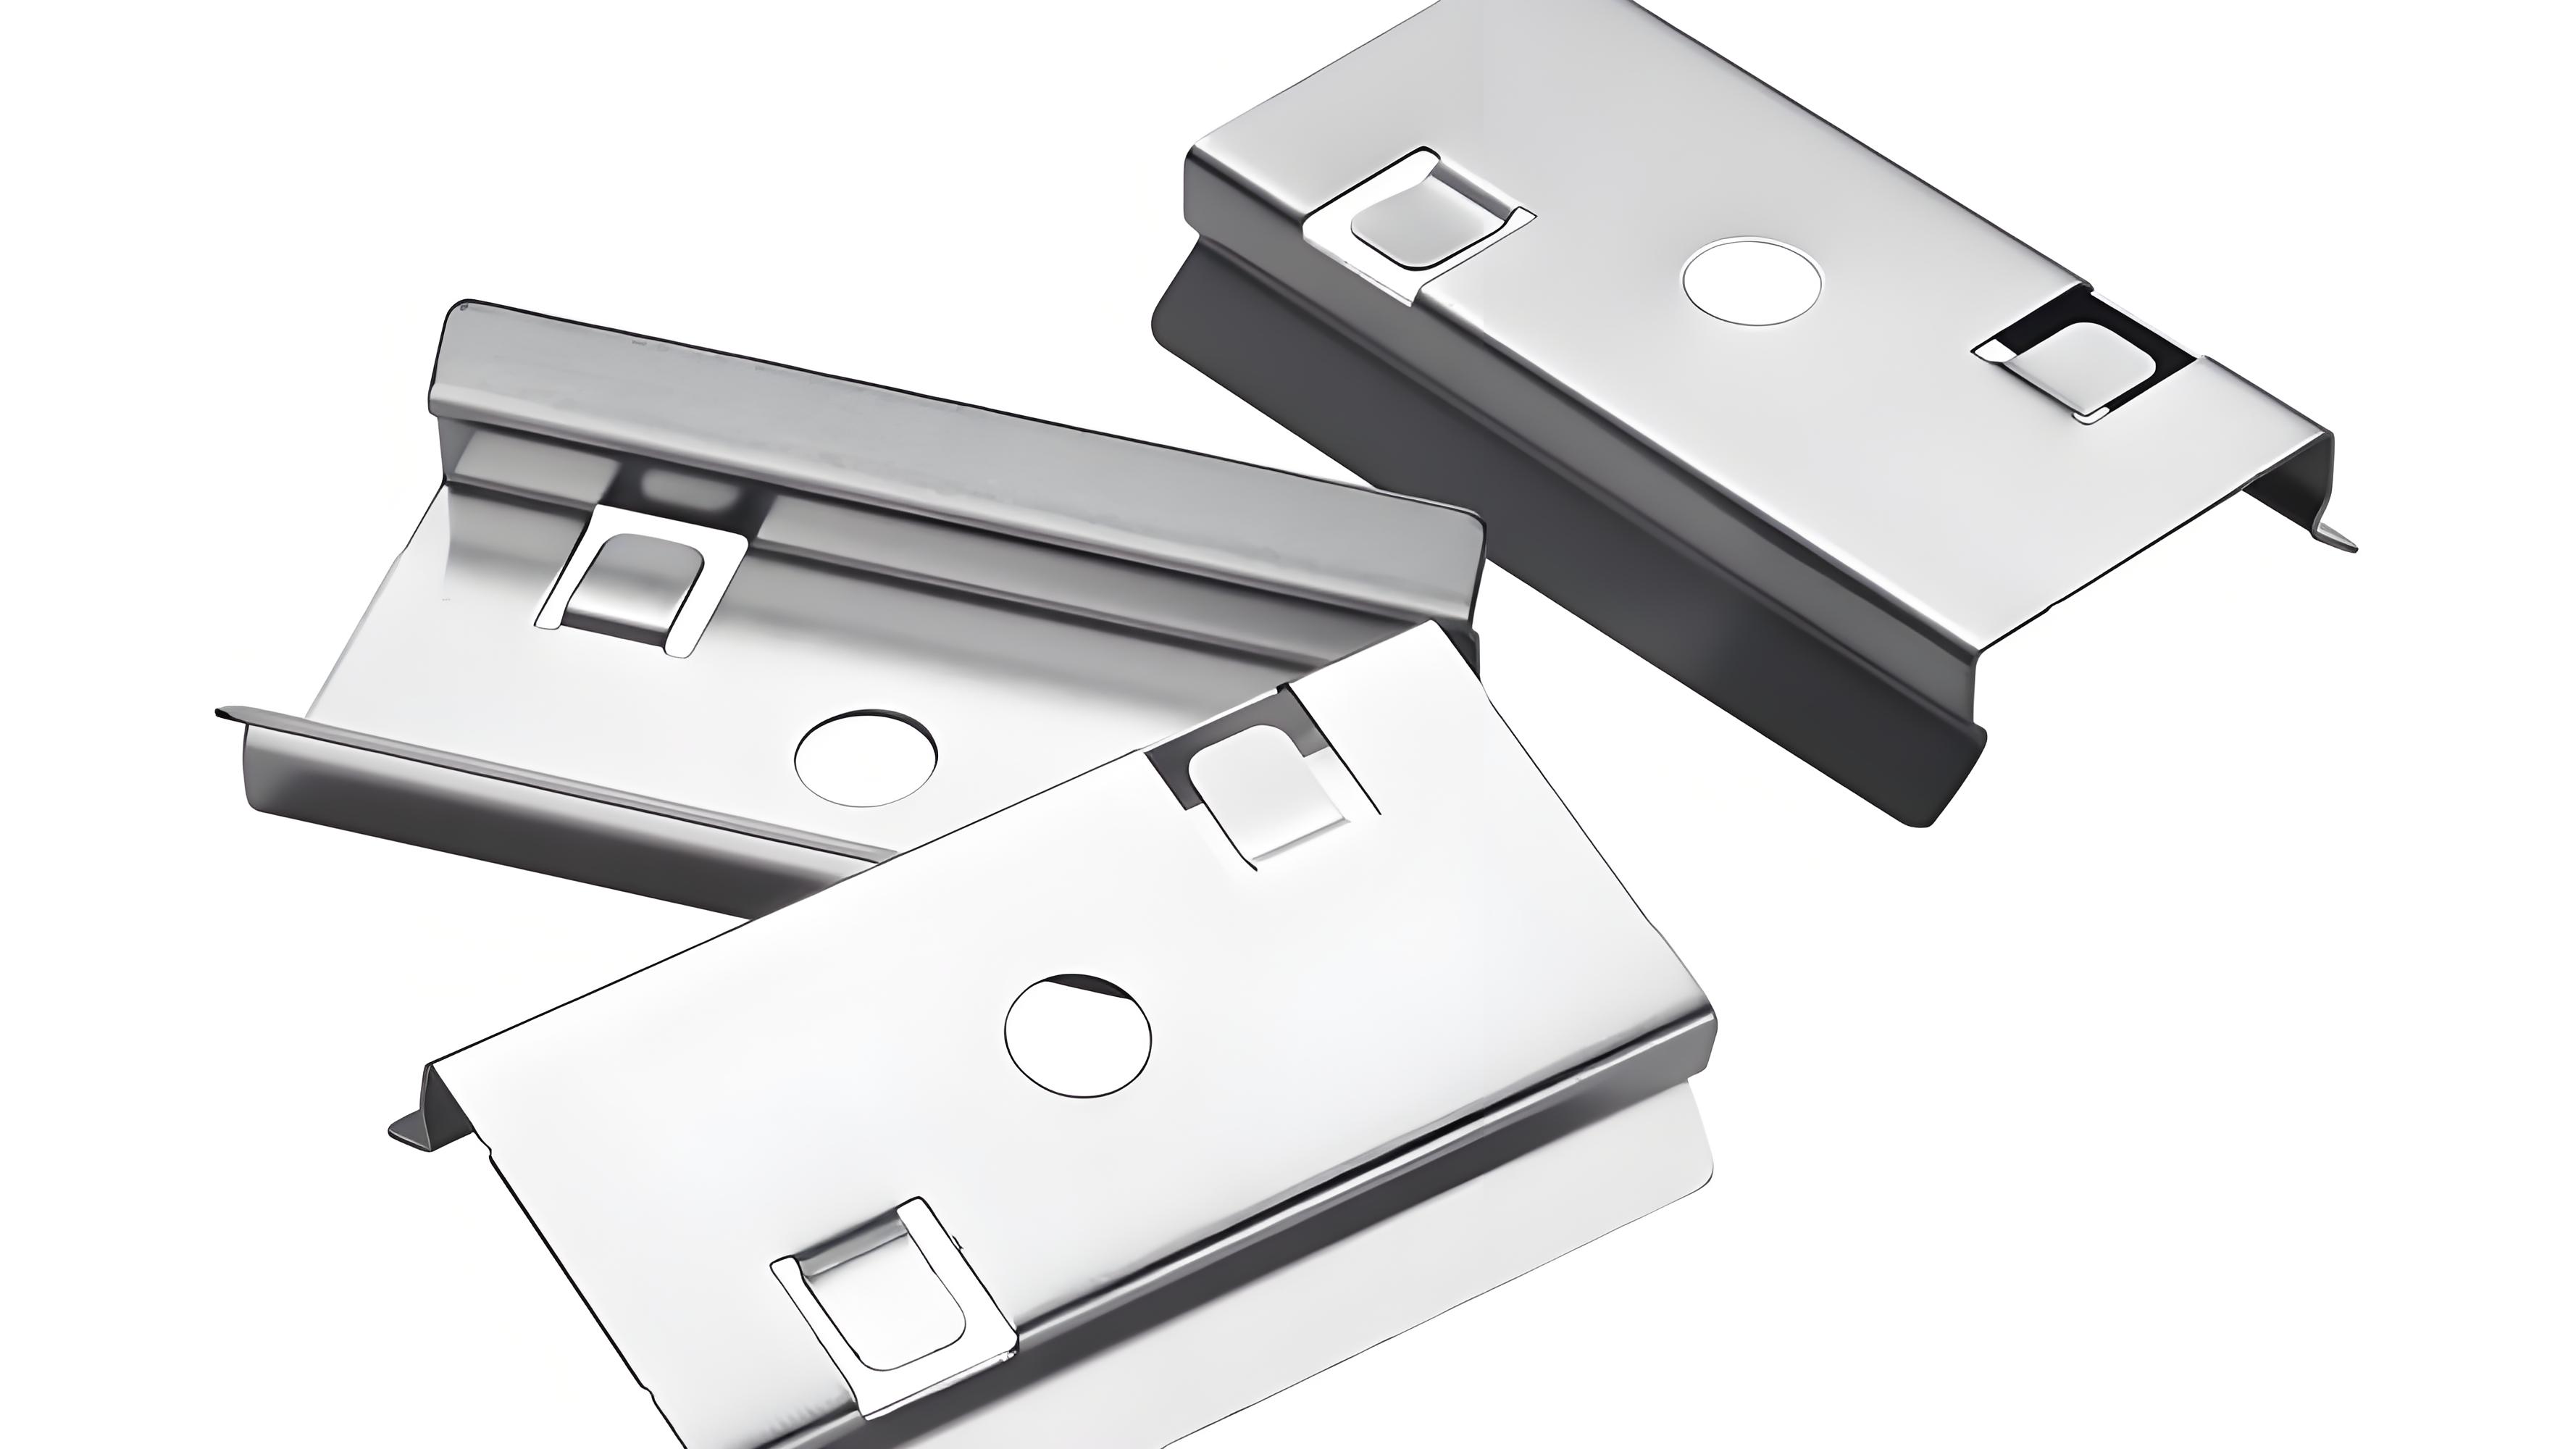
Punching sheet metal parts can be complex, so to make it easier to incorporate into your next project, here is a list of helpful manufacturability reminders to consider during the design process. These guidelines can help you manage project costs and achieve high part quality.
The additional punching design guidelines below can be a useful resource in achieving dimensionally accurate and quality punched parts.
| Tool Station Diameter | Space Required Between Features |
|---|---|
| 0.500 in. (12.7mm) | 0.250 in. (6.35mm) |
| 1.250 in. (31.75mm) | 0.625 in. (15.875mm) |
| 2.000 in. (50.8mm) | 1.000 in. (25.4mm) |
| 3.500 in. (88.9mm) | 1.750 in. (44.45mm) |
| 4.500 in. (101.6mm) | 2.250 in. (57.15mm) |
Our sheet metal fabrication services offer fast turnaround times, high quality, and competitive pricing for both prototyping and production needs. With our digital manufacturing approach, you get real-time pricing and DFM feedback before you commit.
Get Instant Quote

Upload your 3D CAD file and select your material preferences.

Receive real-time pricing and design for manufacturability feedback.

Once approved, we begin manufacturing your parts immediately.

Parts are shipped directly to your door with real-time tracking.
Upload your CAD file and share finish requirements such as color, coating, texture, or marking. We will review the details and help you move from prototype to production.